Hey there, let’s cut to the chase—if you’re in rapid plastic prototyping, you already know support removal is the annoying, make-or-break step that can turn a perfect 3D print or CNC-machined prototype into a post-production disaster. I’ve been on this end for 7+ years, running a shop that cranks out prototypes for startups, medical teams, even consumer product brands (yes, we’ve tackled every single wacky support structure you can imagine), and I’m here to tell you it’s not just about grabbing a pair of pliers and yanking away. It’s a whole process, and mess it up, and you’re staring at a scrapped part that cost you 3 days of lead time and the client’s last minute for a trade show. Rapid Plastic Prototyping
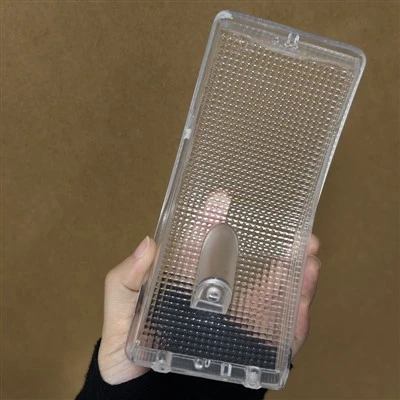
First, let’s start with why support structures even exist here. Rapid prototyping uses two main methods for plastic parts these days: FDM (fused deposition modeling) and SLA (stereolithography) 90% of the time, plus we dabble in SLS too, but that’s less support-heavy. For FDM, if your part has overhangs steeper than 45 degrees, those can’t hang in mid-air while the plastic filament melts—you need a breakaway or soluble support to prop that up. SLA uses liquid resin, so overhangs, enclosed cavities, tiny internal features? Resin would get trapped or collapse mid-cure, so you print with a second support material that’s made to come off easy. The key here is matching the support to the material, not just using one-size-fits-all. I’ve seen new prototypers slap generic supports on a medical part and then can’t get them out without scratching the biocompatible surface—oops.
Let’s break down how we actually handle this, step by step, no jargon, just the stuff that works for our shop. First, we don’t even touch the part until it’s fully post-processed from the build. For FDM parts, that means letting it cool completely (we learned this the hard way—pulling a hot support off a ABS prototype = warped part that’s useless). For SLA, we give it a 24-hour post-cure in the UV chamber, and soak it in isopropyl alcohol for 2 hours to get rid of all the uncured resin trapped on the support interfaces. Skip that step, and the support is fused to the part like glue.
Next, we size up the support type—this is non-negotiable. If it’s breakaway support (the cheap, hard stuff that snaps like a toothpick), we use flush cutters with super fine tips, not household pliers. Those pliers leave gnarly marks on the part, and if you squeeze too hard, you’ll crack a thin wall or a tiny feature like a snap fit tab. We hold the part steady in a soft jaw vise (we line the jaws with silicone so no scratches) and snip from the base of the support, not halfway up—halfway snags. For areas that are super tight, like under a small overhang, we use a dental pick. Yeah, a dental pick—they’re small, have a sharp point that doesn’t mar plastic, and we can get into gaps that pliers will never reach. I keep a whole tray of them in the post-production area, along with different grit sandpaper (220 for heavy leftover marks, 800 for final polish) and rubbing compound for when we need that showroom finish.
Then there’s the tricky one: soluble support. This is for SLA parts where overhangs are really delicate, or internal cavities—you can’t get a pliers in there. We use two types of soluble support: PVA (polyvinyl alcohol) for FDM, and support resin specifically for SLA. For these, we don’t cut anything first. We toss the whole part (support and all) into a heated water bath, set to 120 degrees F, and let it soak. How long? Depends on the size of the part—small prototype with a single cavity? 4 hours. Big part with multiple internal channels? 24 hours max. We shake the bath every hour to help the solvent break down the support faster, and if there’s still a tiny bit left in a super narrow gap, we add a drop of dish soap to the water. It works like a charm, and we’ve only had 2 issues with this method in 7 years—once when the client ordered a part that needed a 3D printed thread, and the soluble support got stuck in the threads. We had to use a syringe to squirt soapy water into each thread, which took an extra hour, but we didn’t ruin the part.
Wait, what about parts with tiny, internal support structures? Like a prototype for a drone arm with a hollow channel, or a medical part that needs a lattice inside? We don’t soak those in a water bath—instead, we use compressed air (like the stuff you use for your computer keyboard) on low pressure, plus those dental picks. For super stubborn support in tiny holes, we drill a micro-hole (1mm max) into the part to flush out the residue, then cap it later. Drill bits for plastic, not metal—no shavings, no scratches.
But here’s the real secret sauce we learned from 100+ client horror stories: we design the support with the CAD team, not just the 3D printer operator. If a client sends us a part file, we don’t just hit “print” and call it a day—we flag areas where support removal will be a pain. Last month, a startup sent us a phone case prototype with a 0.5mm overhang on the side. The original support design would have left a super thick mark that would have been impossible to sand smooth. We talked them into tweaking the overhang angle by 10 degrees, and used a thinner support structure that came off with just a dental pick, no sanding needed. That’s the stuff that saves us time and makes clients happy—we’re not just a print shop, we’re problem solvers.
Now, let’s talk about the mistakes we’ve made, so you don’t have to. Early on, we tried speed running support removal for a rush order. We pulled a hot FDM part, yanked the support off with pliers, and the part warped so bad it couldn’t fit into the client’s mold prototype. Cost us a re-print and a late fee—we still have that client’s feedback note: “please take your time.” Another time, we used a generic soluble support for a medical prototype that needed to be biocompatible. The leftover PVA had impurities, and we had to re-soak it for 12 hours, which pushed back their deadline by 2 days. Now we test every support material for biocompatibility if the client needs it, no exceptions.
What about CNC prototyping? Wait, most people forget that rapid prototyping isn’t just 3D printing—we do CNC too, and support removal there is totally different. For CNC, we use custom tool paths that leave small “support tabs” to hold the part in place while it’s being milled. We remove those tabs with a band saw for big parts, or a small file for tiny ones, then sand the edge smooth. No dental picks there, but the same rule applies: don’t rush, or you’ll nick the part edge.
Here’s the thing: support removal isn’t a afterthought. It’s the final step that makes the prototype actually usable. A perfect 3D print with a bunch of leftover support marks is just a paperweight. A prototype with clean, smooth surfaces is what gets investors excited, what passes functional testing, what turns into a real product.
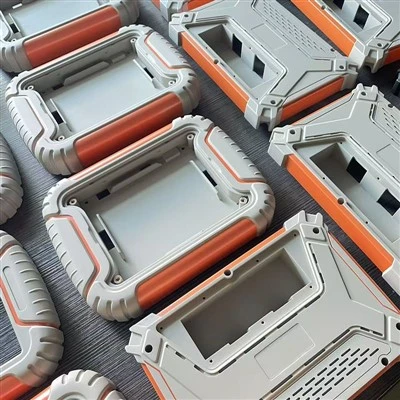
If you’re someone who’s tired of scrapping prototypes because of bad support removal, or you’re a startup that needs to nail a trade show prototype in 3 days, hit us up. We don’t do one-size-fits-all, we don’t rush parts, and we’ve fixed more support messes than we can count. We can walk you through CAD tweaks to make support removal easier, use the right tools and materials for your part, and get you a prototype that’s ready to go, no post-processing headaches for you.
Precision CNC Machining References
- Campbell, R.I. (2018). Support Structures for Additive Manufacturing: A Review of Design Strategies and Post-Processing Methods. Rapid Prototyping Journal, 24(5), 892-905.
- Gibbs, G. & Patel, M. (2021). Post-Processing Techniques for FDM and SLA Plastic Prototypes: Minimizing Surface Defects and Support Residue. Journal of Manufacturing Processes, 67, 412-421.
- Lee, S. & Park, J. (2020). Soluble Support Systems for Stereolithography: Material Compatibility and Soaking Time Optimization. Additive Manufacturing, 35, 101389.
Shenzhen Multi-Wins Precision Technology Co., Ltd.
As one of the most professional rapid plastic prototyping manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please feel free to buy customized rapid plastic prototyping made in China here from our factory. Also, quotation is available.
Address: 1 Phase, Yi’an City Central Garden, Longfei Avenue, Longgang District, Shenzhen, GD, China. 518100
E-mail: info@multi-wins.com
WebSite: https://www.multi-wins.com/
